HT Energy has built and commissioned an in-house RO water treatment skid rated at 500 liters per hour, purpose-built to feed our chemical cleaning operations.
RO water quality drives the outcome of every chemical cleaning job — it sets the baseline for chemical dosing accuracy and determines whether a system passes final cleanliness verification. Sourcing it externally meant depending on third-party suppliers, with the usual risks: inconsistent water quality between batches, and schedule exposure whenever a supplier couldn’t deliver on time.
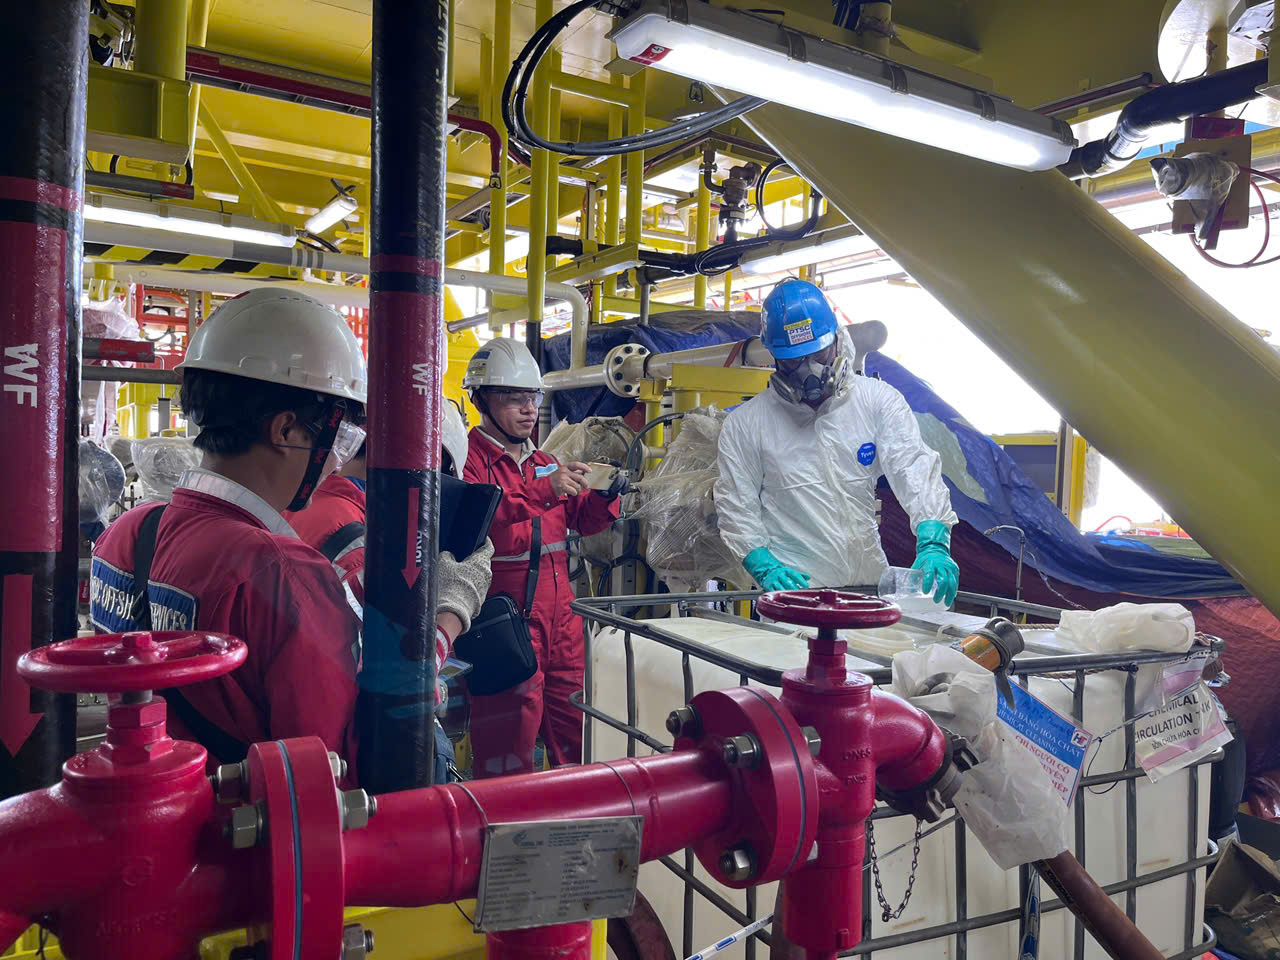
The new skid runs pre-filtration, RO membrane housings, a high-pressure feed pump, and a control panel with pressure monitoring, all mounted on a portable steel frame with lifting points and forklift pockets for site or offshore mobilization.
It’s already in service at LDV-A, supporting the offshore pre-commissioning campaign.
This sits alongside our other in-house equipment builds, including the 180,000 SCF/hr N₂ liquid-to-gas converter pump unit — part of a deliberate push to control the equipment that sits on our critical path instead of renting or subcontracting it.